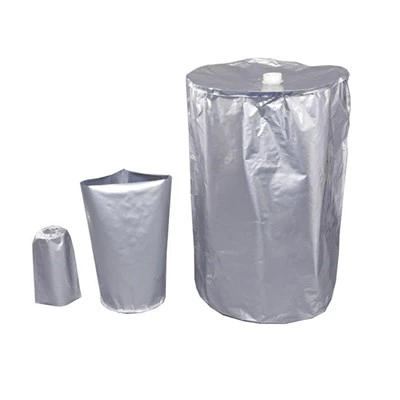
Overview
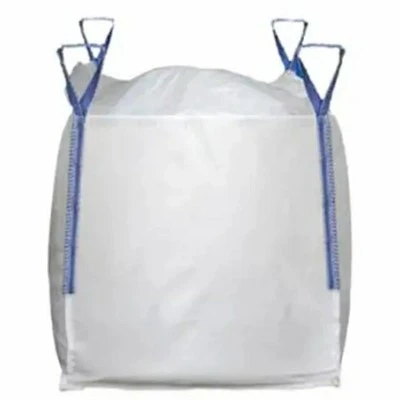
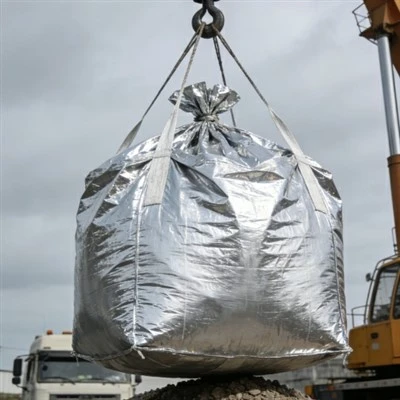
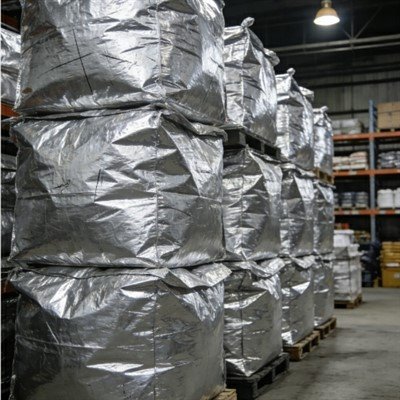
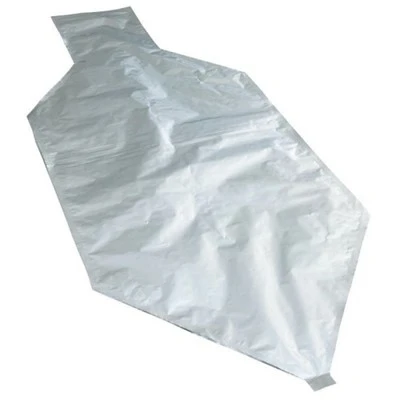
Aluminum foil bulk bags are a type of packaging product primarily composed of aluminum foil. Characterized by properties such as moisture resistance and corrosion resistance, they are widely utilized across a diverse range of industries.
Scope of Application Analysis:
1. Chemical Industry: Many raw materials and finished products used within the chemical industry require specialized protective measures to guard against the adverse effects of moisture and chemical reactions. Consequently, aluminum foil bulk bags have emerged as an ideal packaging choice due to their superior sealing capabilities and corrosion resistance.
2. Construction Materials Industry: In the construction sector, the handling of materials-such as cement and various other building supplies-necessitates waterproof and moisture-proof protection to shield them from environmental exposure. Aluminum foil bulk bags not only ensure the quality and performance stability of these materials but also serve to extend their usable lifespan.
3. Applications in Other Fields: Aluminum foil bulk bags are also extensively employed in the transportation and storage of specific specialized products within sectors such as the food and pharmaceutical industries.
Advantages of Application in High-Temperature Environments:
Given aluminum foil's inherent resistance to high temperatures, these bulk bags are able to maintain their structural integrity even when deployed in high-temperature environments. This capability effectively prevents cargo from sustaining moisture damage and safeguards against adverse reactions with other substances.